Integrated Checkweigher & Metal Detector Combination Systems
Explore China’s leading industrial-grade combined checkweigher and metal detector systems engineered for zero-defect production lines, compliant with FDA, HACCP, BRCGS, and IFS standards.
Combined Conveyor Metal Detector and Checkweigher for Food Industry
Juzheng Conveyor Belt Metal Detector & Checkweigher Combo Machine Food Grade Steel
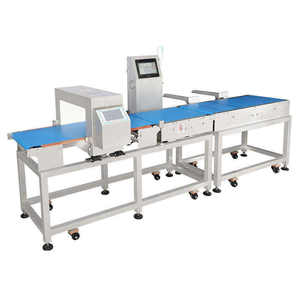
Industrial Food Combo Metal Detector and Checkweigher Machine
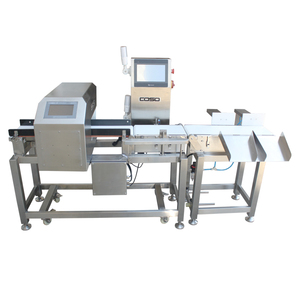
Industrial Combo Metal Detector and Checkweigher Machine Made In China
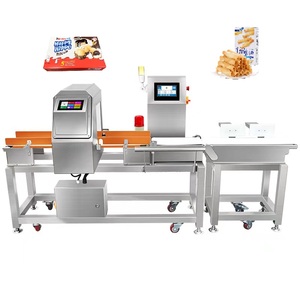
High Accuracy Touch Screen Checkweigher Metal Detector Combo System IP55 SS
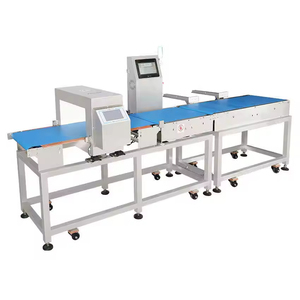
Compact Space-Saving Metal Detector Checkweigher Combo System
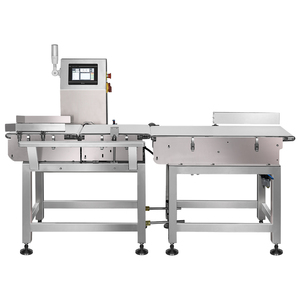
Customizable Automatic Stainless Steel Metal Detector & Weight Scale Combo OEM/ODM
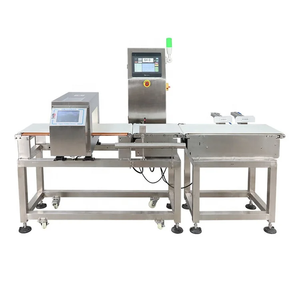
De Metales Metal & Check Weigher Combination Unit With Dual-Channel Rejector
Modern Quality Assurance: Why Integrated Checkweigher & Metal Detector Systems are Essential
In high-speed food processing, pharmaceutical manufacturing, and consumer packaged goods (CPG) packaging lines, operational efficiency and quality compliance are non-negotiable. Historically, quality managers were forced to install standalone conveyor belt metal detectors and separate inline checkweighing scales. This traditional setup required extensive floor space (often exceeding 3.5 meters of linear conveyor length), complex multi-vendor software integration, redundant electrical control cabinets, and elevated maintenance overhead.
As a leading China checkweigher and metal detector combo factory and supplier since 1996, we have pioneered the integration of electromagnetic metal detection with high-speed strain gauge and Electromagnetic Force Restoration (EMFR) dynamic checkweighing into a singular, compact, mono-frame architectural system. By combining both critical control point (CCP) functions into a unified footprint (reducing conveyor length by up to 45%), global manufacturers achieve superior operational control, zero product giveaways, absolute foreign contaminant elimination, and full compliance with FDA 21 CFR Part 11, HACCP, BRCGS, and IFS auditing standards.
Information Gain Key Takeaway for Procurement Officers
Integrating a combined metal detector checkweigher machine cuts capital expenditure (CapEx) by 25-35% compared to purchasing separate systems, while reducing line setup footprint and unifying data reporting through a single 10-inch Siemens/Omron industrial HMI touch interface.
Key Technologies Driving Combo System Performance
Our combo systems combine cutting-edge Digital Signal Processing (DSP) with ultra-sensitive strain gauge load cells to provide unmatched accuracy and detection sensitivity.
Dual DSP Signal Processing
Independent Digital Signal Processors handle metal detection and dynamic weight processing simultaneously. Phase discrimination algorithms suppress product effect caused by high-moisture or conductive salted foods.
EMFR & Precision Strain Gauge Load Cells
Utilizing high-end sensors sourced from world-class suppliers, our dynamic weighing bridge achieves up to ±0.1g accuracy at speeds of up to 250 packs per minute with automatic zero-tracking and dynamic belt compensation.
Tri-Frequency Metal Detection
Capable of simultaneously detecting Ferrous (Fe), Non-Ferrous (NFe), and Stainless Steel (SS316) contaminants down to 0.4mm Fe, 0.6mm NFe, and 0.8mm SS, even inside metallized film foil packaging.
Smart Dual Rejector Mechanism
Equipped with dual independent rejection channels (Pneumatic Pusher, Air Blast, Drop-Belt, or Flipper Arm) to separate weight-out-of-spec packages from metal-contaminated packages into lockable bins.
IP65 / IP69K Sanitary Construction
Constructed entirely from SUS304 or SUS316L food-grade stainless steel with toolless quick-release conveyor belts for effortless high-pressure washdown hygiene control in raw meat and dairy environments.
Industry 4.0 & Data Integration
Supports Modbus TCP, Ethernet/IP, OPC-UA, and USB data export. Real-time SPC statistics, weight distribution histograms, and audit trail logs ensure seamless ERP/MES integration.
Technical Specification & Selection Overview
Compare performance specifications across our standard industrial combo metal detector and checkweigher series.
| System Model | Weighing Range | Dynamic Accuracy | Max Belt Speed | Fe / NFe / SS Sensitivity | Sanitary Rating |
|---|---|---|---|---|---|
| Combo Micro-Pack CS-100 | 2g – 300g | ± 0.05g – 0.1g | up to 280 pcs/min | Fe: 0.3mm / NFe: 0.5mm / SS: 0.7mm | IP54 / IP65 Stainless |
| Combo Standard Food CW-1500 | 10g – 1500g | ± 0.15g – 0.3g | up to 180 pcs/min | Fe: 0.5mm / NFe: 0.8mm / SS: 1.2mm | IP65 Washdown SUS304 |
| Combo High-Pay-Load CW-6000 | 100g – 6000g | ± 0.5g – 1.0g | up to 110 pcs/min | Fe: 0.8mm / NFe: 1.2mm / SS: 1.8mm | IP65 Heavy Industrial |
| Combo Heavy-Duty Box CW-15K | 500g – 15000g | ± 2.0g – 5.0g | up to 60 pcs/min | Fe: 1.2mm / NFe: 1.8mm / SS: 2.5mm | IP55 Modular Conveyor |
| Customized Foil-Pack Series | Custom OEM | Tailored to Line | Variable Frequency Drive | Multi-Phase Foil-Specific DSP | IP69K Harsh Washdown |
Why Partner With Our China Manufacturing Facility?
Combining 28+ years of packaging and inspection machinery engineering with world-class component sourcing and international compliance certificates.
28+ Years of Direct Manufacturing
Established in 1996, our factory operates extensive precision machining facilities. We control every stage of fabrication from frame laser cutting and CNC machining to electrical wiring and dynamic calibration.
Global Compliance & Certification
Our operations are certified under ISO 9001:2015 (Quality Management) and ISO 14001:2015 (Environmental Management). Every machine carries full CE certification and complete electrical documentation for easy site validation.
World-Class Component Eco-System
We build long-term operational stability into our equipment by sourcing critical pneumatics, electronics, and sensors exclusively from global industry leaders, including Siemens, Schneider Electric, Festo, Omron, SMC, and LG.
2-Year Warranty & Global Service
We provide a comprehensive 2-year warranty on all structural and electronic components. Certified field technicians deliver on-site installation, staff training, and lifetime remote diagnostic support to clients in over 50 countries.
Future Development Trends in Checkweighing & Metal Detection
Anticipate technology shifts to maximize your equipment ROI over the next decade.
1. AI-Driven Signal Filtering & Auto-Tune
Traditional metal detectors require manual operator calibration to filter out product effect from high-salt or frozen foods. Modern combo machines feature artificial intelligence algorithms that continuously learn and dynamically adjust phase angles in real-time, drastically reducing false rejection rates.
2. Seamless Industry 4.0 Connectivity
Procurement teams are shifting toward smart factories where checkweighers automatically send feedback signals to upstream multihead weighers or volumetric auger fillers. This closed-loop control system automatically adjusts filling quantities, eliminating costly product giveaway.
3. Multi-Simultaneous Frequency Scanning
Single or dual-frequency metal detection is being replaced by multi-simultaneous frequency spectrum scanning technology. This allows detection of spherical and wire-shaped stainless steel contaminants across varying moisture levels without recalibration.
4. Toolless Hygienic Modularization
Strict food safety regulations dictate that cleaning down times must be minimized. Next-generation combo systems feature toolless belt disassembly, open-frame stainless steel channels, and IP69K washdown enclosures for rapid sanitation cycles.
Frequently Asked Questions for Overseas Buyers
Clear answers to technical, operational, and shipping questions regarding combo checkweigher and metal detector systems.
Why should I choose a checkweigher and metal detector combo instead of standalone machines?
A combo unit saves up to 45% of floor space on your packaging line, reduces equipment acquisition cost by 25-35%, unifies your operational software into a single touch-screen interface, and simplifies audit logging for FDA, HACCP, BRCGS, and IFS compliance.
How does the system distinguish between a weight reject and a metal detection reject?
Our combined systems feature independent dual-reject mechanisms (such as dual pneumatic pushers or air jets) leading to two separate, key-locked reject catch bins. This guarantees that metal-contaminated products are never mixed with under/over-weight products.
What metal detection sensitivity can be achieved on packaged food lines?
Typical sensitivity ranges from 0.3mm to 0.8mm for Ferrous (Fe), 0.5mm to 1.2mm for Non-Ferrous (NFe), and 0.6mm to 1.5mm for Stainless Steel (SS316), depending on aperture height, product size, and moisture content (product effect).
Can the combo machine handle products packed in aluminum foil or metallized film?
Yes. We offer specialized multi-frequency metal detection heads engineered to work through aluminum foil bags, as well as magnetic induction detectors designed specifically for inspect-after-canning applications.
What after-sales service and spare parts support do you offer international buyers?
We provide a full 2-year warranty. Replacement parts (such as belts, sensors, load cells, and pneumatic valves) are shipped worldwide via express air freight within 24-48 hours. Remote video engineering assistance and on-site commissioning technicians are readily available.
How do I determine the right belt width and machine length for my production line?
Our engineering team selects belt width and length based on your maximum package dimensions (L x W x H), total package weight, required throughput speed (packages per minute), and sanitary washdown level. Contact us today for custom CAD drawings.
Ready to Upgrade Your Packaging Line Quality Control?
Get complete engineering specifications, custom CAD layout proposals, and factory-direct wholesale pricing from China’s premier checkweigher and metal detector combination system manufacturer.