High-Performance Packaging & Bagging Systems
Explore our export-grade packaging machinery range—engineered for precise viscosity control, powder dosing, and multi-format pouch sealing.
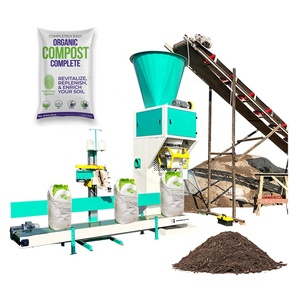
25kg 50kg Mulch Compost Irregular Shaped Pieces Bag Sealing Packing Machine
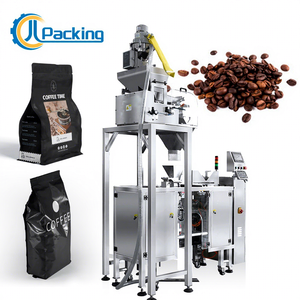
Doypack Multi-Function Pouch Packing Food Granule Automatic Bag Packaging Machine
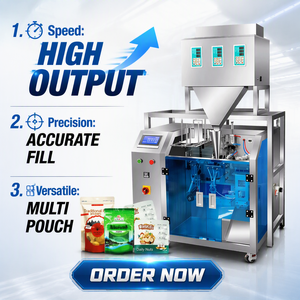
Coffee Beans Gusset Stand-up Bag Pick Fill Seal Vertical VFFS Packaging Machine
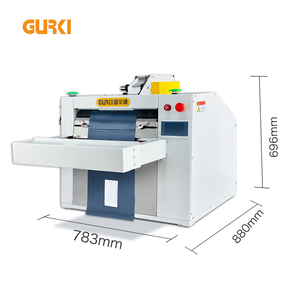
High Speed Automatic Tabletop Bagging Machine With Wrapping & Gluing Functions
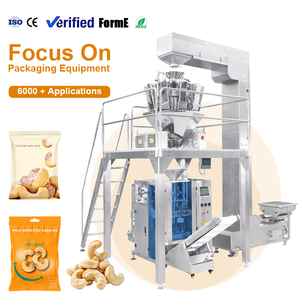
Food Grade Automatic Almonds Cashews Peanuts Back Seal Pillow Bag Packing Machine
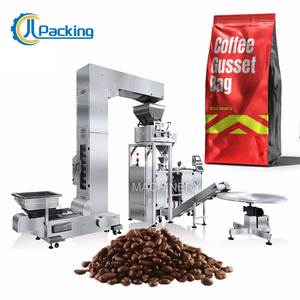
Doypack Roasted Coffee Bean Gusset Bag Ziplock Pouch Automatic Packing Machine
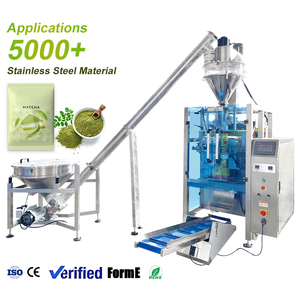
High Precision Automatic Vertical Gusset Bag Matcha Powder Walnut Powder Packing Machine
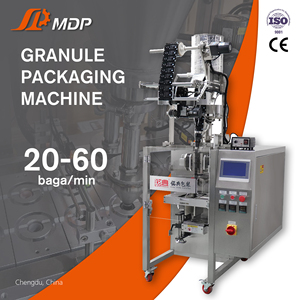
Multi-Function Automatic Vertical Granule & Liquid Pouch Packaging Machine
Engineering Excellence in Honey Sachet Packaging Technology
In the global fast-moving consumer goods (FMCG) and nutraceutical markets, single-serve honey sachets and stick packs have transformed from convenience options into high-margin product categories. Driven by rising consumer demand for portable energy, organic dietary supplements, fast-food condiment pouches, and premium Manuka honey doses, food processors worldwide require packaging systems capable of handling non-Newtonian, high-viscosity liquids with absolute accuracy.
As China’s premier honey sachet packaging machine supplier and global exporter, our manufacturing plant integrates over 28 years of mechanical design, pneumatic engineering, and digital automation. We engineer turnkey vertical form-fill-seal (VFFS) and 4-side seal sachet packaging machines specifically configured to overcome the fluid-dynamic challenges of natural raw honey, processed syrups, and liquid propolis.
Honey exhibits non-Newtonian shear-thinning and temperature-dependent viscosity characteristics (ranging from 2,000 cPs at 40°C to over 10,000 cPs at ambient room temperature). Standard liquid fillers suffer from severe stringing, tailing, volume drift, and seal contamination. Our systems integrate thermostatically controlled jacketed hoppers, pneumatic anti-drip rotary valves, and servo-actuated piston pumps to guarantee continuous seal integrity at speeds up to 240 sachets/min across multi-lane configurations.
Verified Direct Manufacturer Standards
Certified under ISO 9001:2015 Quality Management Systems and ISO 14001:2015 Environmental Standards. Every export machinery unit carries full CE Certification compliant with EU Machinery Directive 2006/42/EC. Operating with top-tier international componentry: Siemens PLC, Festo Pneumatics, Schneider Electrics, and Omron PID Temperature Control.
Overcoming Core Technical Challenges in Viscous Liquid Packaging
Packaging liquid honey into airtight 3-side, 4-side, or stick pack sachets requires specialized mechanical sub-assemblies. Standard liquid dosing mechanisms fail due to honey’s sticky consistency, surface tension, and crystallization behaviors. Below are the key engineering innovations incorporated into our honey sachet packaging machines:
1. Thermostatically Heated Jacket Hopper
Honey's viscosity drops significantly when warmed safely between 35°C to 45°C without altering its enzymatic properties or taste. Our hoppers feature double-walled water jackets with digital PID temperature loops, keeping honey fluid for consistent filling.
2. Positive Cut-Off Anti-Drip Nozzles
Drop-tailing onto pouch sealing areas causes channel leaks and shelf-life failure. Our proprietary blow-back pneumatic shut-off nozzles instantly sever liquid honey flow at the microsecond dosing completes, ensuring zero film margin contamination.
3. Food-Grade Sanitary Contact Materials
All product-wet contact areas are constructed from AISI 316L Stainless Steel with mirror-polished internal surfaces (Ra < 0.4µm). Designed for rapid CIP (Clean-In-Place) sanitation to comply with FDA, EHEDG, and EU food hygiene standards.
Technical Benchmark Comparison: Honey Sachet Packaging Series
Compare operational parameters across our flagship single-lane and multi-lane liquid packaging equipment lines.
| Machine Specification | Single-Lane 4-Side Sachet | Multi-Lane Stick Pack (4-10 Lanes) | Rotary Pre-Made Doypack Line |
|---|---|---|---|
| Target Packaging Format | Flat 3-Side / 4-Side Sachet | High-Speed Single-Serve Stick Pack | Stand-up Zip Pouch / Doypack |
| Dosing Range (Volume) | 1ml - 100ml | 2ml - 30ml (Expandable) | 50ml - 1000ml |
| Filling Precision | ±0.5% (Servo Piston) | ±0.3% (Individual Servo Pumps) | ±0.5% (Flowmeter / Piston) |
| Output Capacity | 30 - 80 packs/min | 160 - 450 packs/min | 20 - 55 pouches/min |
| Film Compatibility | PET/AL/PE, PET/NY/PE, Paper/AL/PE | Laminated Foil, Recyclable Mono-PE | Pre-formed Laminated Pouches |
| Temperature Control | Dual Digital PID (Omron) | Multi-Zone Independent PID | PLC-Integrated Thermal Bars |
| Air Consumption | 0.3 m³/min (0.6 MPa) | 0.8 m³/min (0.8 MPa) | 0.5 m³/min (0.6 MPa) |
| Clean-In-Place (CIP) | Quick-Release Sanitary Tri-Clamp | Automated CIP Flushing Manifold | Automated Tank & Line CIP |
Future Procurement Trends in Honey & Viscous Packaging
How smart automation, sustainable films, and digital quality assurance are redefining international honey processing lines.
1. Transition to Eco-Friendly Recyclable Mono-Films
Global environmental regulations (such as the EU Packaging and Packaging Waste Regulation - PPWR) are forcing brand owners to abandon traditional aluminum foil laminates. Modern honey sachet machines must operate with thinner, heat-sensitive recyclable mono-materials (like MDO-PE or PP). Our next-generation sealing jaws utilize pulse-heating thermal profile controllers that prevent film burn-through while guaranteeing airtight seals.
2. Industry 4.0 IoT Integration & Remote Diagnostics
International buyers purchasing packaging equipment from China prioritize uptime and operational transparency. Our machines feature EtherNet/IP and OPC-UA connectivity, enabling remote diagnostics, real-time yield tracking, automated OEE reporting, and cloud-based predictive maintenance alerts directly to plant manager smartphones.
3. Precision Micro-Dosing for Nutraceutical Honey
High-value products such as certified UMF Manuka honey, royal jelly, and propolis blends require exact micro-dosing (e.g., 5g to 15g single doses). High-precision servo piston drives eliminate give-away costs, delivering an accuracy margin of ±0.3%, protecting raw material profit margins.
4. Integrated Downstream Secondary Packaging
Modern procurement moves away from standalone pouch wrappers toward complete turnkey lines. Our honey sachet filling systems integrate seamlessly with online vision inspection (checkweighers, leak detectors), automated robotic pick-and-place cartoning units, and outer case packers.
China’s Leading Packaging Machinery Manufacturer & Global Exporter
Combining factory-direct price efficiency with European-grade quality control standards.
1996 Manufacturing Foundation
Over two decades of continuous innovation in automatic liquid, powder, and granule packaging machinery. We operate a state-of-the-art production facility with CNC machining centers for in-house part fabrication.
Exported to 50+ Countries
Our packaging machinery operates across North America, Europe, the Middle East, Southeast Asia, and South America. We provide international shipping compliance, CE documentation, and customs clearance support.
World-Class Brand Components
We build reliability into every machine by integrating world-renowned electronic and pneumatic brands: Schneider Electric, Siemens, Festo, Omron, SMC, and LG/LS.
2-Year Warranty & Lifetime Support
Every exported machine is backed by a full 2-year manufacturer’s warranty, spare parts replacement guarantee, and lifetime remote video technical assistance from senior engineers.
On-Site Engineering Commissioning
Our factory-certified field service technicians travel worldwide to provide on-site machine assembly, operational tuning, maintenance training, and staff safety certification.
Strict Quality Control & Factory FAT
Before shipment, every honey sachet machine undergoes a 72-hour continuous Factory Acceptance Test (FAT) utilizing customer sample film and actual viscous product simulation.
Frequently Asked Questions (FAQ) for Honey Sachet Buyers
Addressing key engineering, operational, and commercial questions for overseas buyers.
Honey viscosity changes significantly with temperature fluctuations. Our machines integrate a thermostatically controlled jacketed feeding hopper combined with high-precision servo-driven piston pumps. The heated jacket maintains honey at a consistent viscosity (typically 38°C–42°C), while the micro-stepping servo motor regulates piston stroke volume to deliver filling precision within ±0.5% regardless of external room temperature changes.
Seal contamination is the leading cause of sachet leakage in viscous filling. We solve this through our proprietary pneumatic positive cut-off nozzles with active suck-back technology. Upon completion of each injection stroke, the filling valve creates a instantaneous negative pressure vacuum, pulling back residual honey drops before the horizontal sealing jaws engage.
Yes. Our machines are designed with modular quick-change formers and flexible stroke adjustment. You can change sachet width by swapping the former tube, and adjust sachet length via the HMI touchscreen (controlled by servo eye-mark tracking). The sanitary 316L stainless steel pump system allows rapid flushing, enabling you to package honey, fruit jams, ketchup, liquid sugar, and cosmetics on the same machine line.
All machines manufactured for export comply fully with CE Directives (Low Voltage & Machinery Safety) and ISO 9001 quality management standards. We customize electrical configurations (such as 380V 3Phase, 220V 3Phase, or 110V Single Phase; 50Hz/60Hz) and install UL/CSA-certified electrical breakers and wiring according to the destination country’s industrial electrical code.
Standard machine manufacturing lead time is 25 to 35 working days following approval of packaging film samples and engineering drawings. For after-sales support, we supply complete machine manuals, FAT testing videos, electrical schematics, and offer 24/7 video technical assistance. Additionally, our field service engineers are available for overseas factory setup and staff training upon request.
The entire liquid pathway features food-grade quick-release sanitary Tri-Clamp connections. Operators can disassemble the piston pump, hopper, and nozzles within 10 minutes without special tools for manual washing. Alternatively, our machines support connection to central Clean-In-Place (CIP) hot water/steam sanitation systems for automated hygienic flushing.
Ready to Elevate Your Honey Packaging Line Efficiency?
Consult with our senior packaging engineers today to receive detailed technical specifications, film testing reports, and a competitive factory-direct quote tailored to your production capacity.
Inquire Now